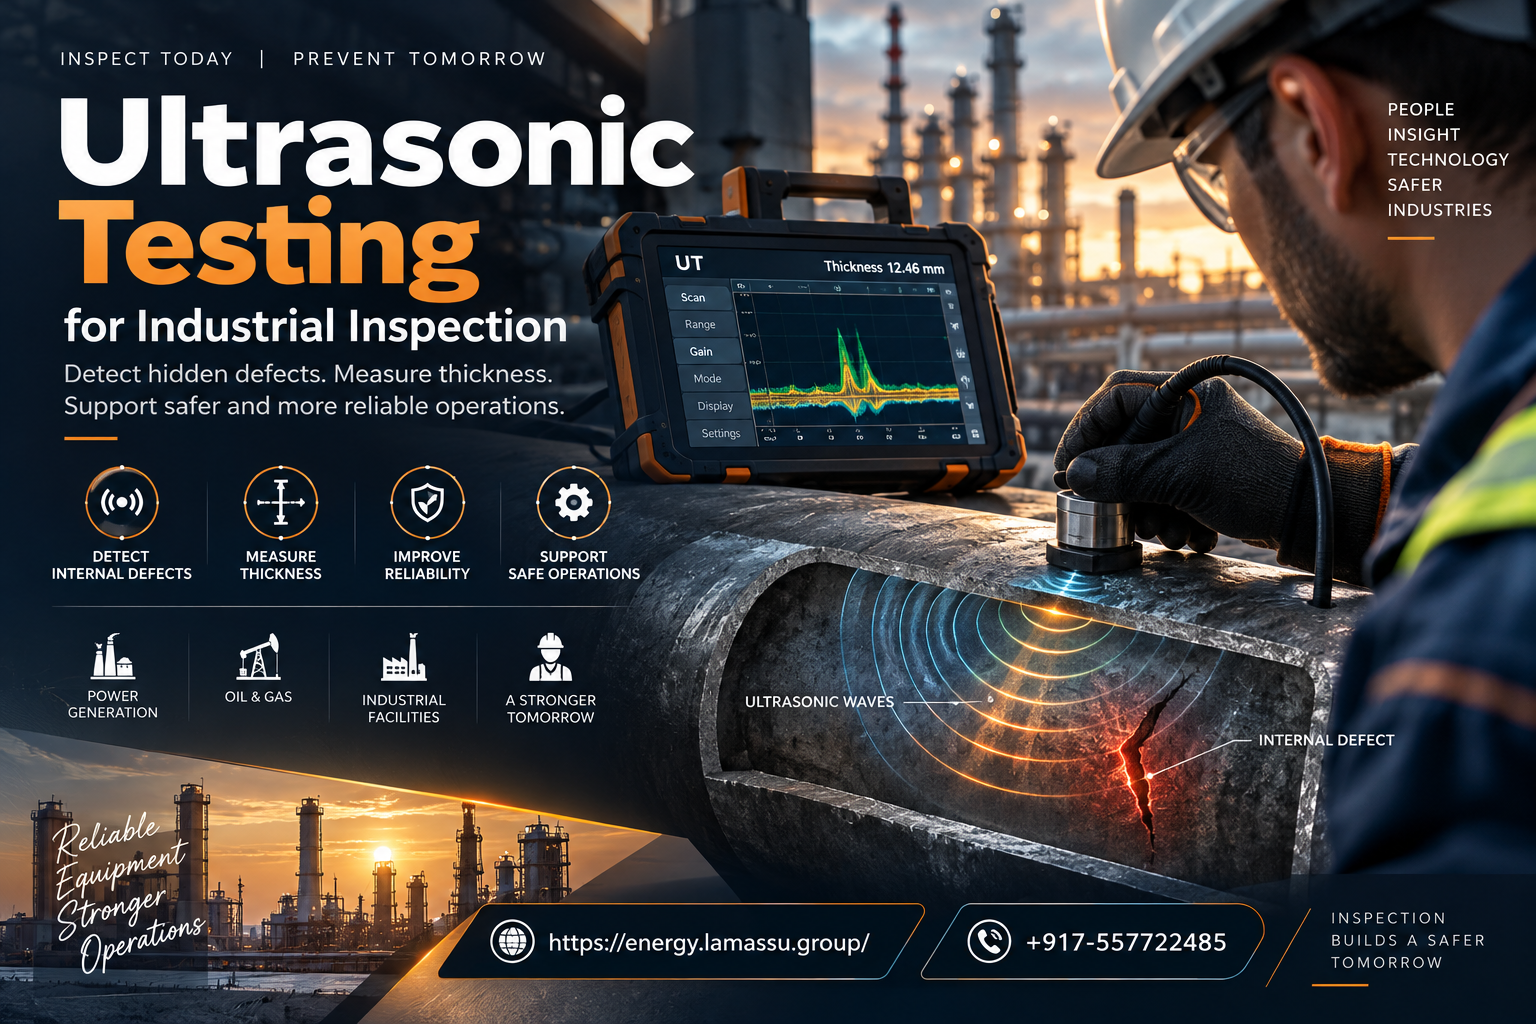
Learn how ultrasonic testing detects hidden defects measures thickness and supports reliable inspection of critical industrial equipment.
What Is Ultrasonic Testing?
Ultrasonic Testing is a non destructive inspection technique that uses high frequency sound waves to examine materials and industrial components without permanently damaging the inspected asset.
The technique is particularly valuable when an inspection team needs information about conditions below the surface or needs to measure material thickness without cutting into the component.
During an Ultrasonic Inspection a probe introduces sound energy into the material. Reflections from material boundaries or discontinuities are received by the equipment and interpreted by a trained technician.
This makes ultrasonic inspection useful for problems such as internal discontinuities wall thickness loss weld evaluation and corrosion monitoring.
Unlike an article comparing all NDT techniques this guide focuses specifically on how ultrasonic inspection works where it provides value what can affect its accuracy and when its limitations should influence the inspection decision.
What Problems Can Ultrasonic Testing Detect?
One of the main reasons facilities use Ultrasonic Testing is the need to investigate conditions that may not be visible during a surface examination.
Depending on the component material inspection setup and expected damage mechanism the technique can help identify or evaluate conditions such as:
- Internal cracking
- Weld discontinuities
- Material thickness loss
- Corrosion-related wall loss
- Lack of fusion in applicable weld inspections
- Certain inclusions or internal reflectors
- Changes in material condition detectable through ultrasonic response
However an ultrasonic indication should not automatically be classified as equipment failure.
The significance of an indication depends on its characteristics the inspection procedure applicable acceptance criteria and engineering evaluation.
How Does Ultrasonic Testing Work?
Most Ultrasonic Testing Methods depend on transmitting high frequency sound energy into a component and analyzing how that energy behaves as it travels through the material.
A typical inspection process may involve:
- Defining the inspection objective
- Selecting the appropriate ultrasonic technique
- Choosing the probe and frequency
- Preparing the inspection surface
- Calibrating the equipment
- Applying couplant when required
- Scanning the inspection area
- Interpreting relevant signals
- Recording inspection results
When sound reaches a material boundary or certain discontinuities part of the ultrasonic energy can be reflected.
The time and characteristics of the returning signal can provide information that helps a qualified technician evaluate the component.
This means reliable UT Testing depends on much more than the testing instrument itself. Calibration probe selection scanning technique component geometry and technician competence can all affect the quality of the examination.
Main Ultrasonic Testing Methods Used in Industry
Different inspection problems require different Ultrasonic Testing Methods. The method should be selected according to the material geometry expected discontinuity and information required.
Pulse Echo Testing
Pulse echo testing sends ultrasonic energy into the component and receives returning echoes using a probe.
The technique can be applied to selected weld inspections material evaluation and thickness measurements.
The travel time and response of the ultrasonic signal help the technician evaluate reflectors within the material.
Phased Array Ultrasonic Testing
Phased Array Ultrasonic Testing uses a probe containing multiple elements that can be electronically controlled to steer and focus the ultrasonic beam.
This capability can provide detailed inspection information across different angles and areas of a component.
Applications may include complex weld examination corrosion mapping and inspection of components where conventional scanning provides limited information.
The additional capability also increases the importance of appropriate setup procedures data interpretation and qualified personnel.
Time of Flight Diffraction
Time of Flight Diffraction or TOFD uses diffracted ultrasonic signals generated around discontinuity tips.
The technique is frequently associated with weld examination and can provide useful information about the location and dimensions of certain discontinuities when applied correctly.
TOFD may complement other ultrasonic techniques rather than replacing them in every inspection.
Through Transmission Testing
Through transmission uses separate transmitting and receiving probes.
A change in the ultrasonic energy received after passing through the material may indicate a condition affecting sound transmission.
The technique requires an appropriate inspection configuration and is used for selected applications rather than being a universal replacement for pulse echo testing.
Ultrasonic Thickness Testing for Material Loss
Ultrasonic Thickness Testing addresses a specific industrial problem: determining remaining material thickness without cutting into the equipment.
The technique measures the travel time of ultrasonic energy through the material. When the appropriate sound velocity is known this information can be used to determine thickness.
Applications include:
- Process piping
- Pipelines
- Storage tanks
- Pressure vessels
- Boiler-related components
- Structural elements
- Other equipment exposed to corrosion or erosion
The ability to take measurements from one accessible side in many applications makes Ultrasonic Thickness Testing particularly useful for in-service equipment.
Using Ultrasonic Thickness Testing for Corrosion Monitoring
Corrosion monitoring is more useful when inspection teams evaluate trends rather than relying on one isolated reading.
A structured thickness monitoring program may include established measurement locations documented readings repeatable procedures and comparison with previous inspection data.
The objective is to understand whether material loss is occurring and how the condition is developing over time.
A typical process is:
Baseline Thickness → Periodic Measurement → Trend Comparison → Engineering Evaluation → Maintenance Decision
This keeps the focus on the actual problem of material loss rather than simply collecting thickness measurements without a decision framework.
Ultrasonic Testing for Weld Inspection
Weld integrity is another important Ultrasonic Testing Application.
Internal weld conditions are not always visible from the surface. Ultrasonic techniques can provide information about certain discontinuities within welded joints when the inspection procedure is suitable for the material geometry and expected defect.
Applications may include evaluating indications associated with:
- Cracking
- Lack of fusion
- Incomplete penetration
- Certain inclusions
- Other relevant weld discontinuities
Detection capability can change depending on defect orientation inspection angle component thickness and material characteristics.
This is why weld inspection should be based on an appropriate procedure rather than assuming that every internal defect will automatically produce an easily identifiable ultrasonic signal.
What Affects Ultrasonic Inspection Accuracy?
Understanding the factors that can affect Ultrasonic Inspection is essential when evaluating results.
Equipment Calibration
Incorrect calibration can affect distance thickness and indication-location information.
Calibration should therefore match the inspection requirements and applicable procedure.
Probe Selection
Probe frequency size angle and type can influence inspection sensitivity penetration and resolution.
The correct probe depends on the material thickness geometry and inspection objective.
Surface Condition
Roughness coatings contamination or irregular surfaces can affect coupling and sound transmission.
Surface preparation requirements should be considered before examination.
Component Geometry
Curved surfaces weld profiles edges and other geometric features can create ultrasonic responses that require careful interpretation.
Material Properties
Grain structure attenuation and other acoustic characteristics can make some materials more challenging to inspect.
Defect Orientation
The orientation of a discontinuity relative to the ultrasonic beam can influence its detectability.
Temperature
Component temperature can affect ultrasonic behavior couplant performance and inspection setup and should be considered where relevant.
Technician Competence
The technician must distinguish meaningful indications from geometry-related or non-relevant signals.
This is one of the reasons qualified personnel are critical to reliable UT Testing.
Benefits of Ultrasonic Testing for Industrial Equipment
When selected for an appropriate inspection problem Ultrasonic Testing offers several important advantages.
Internal Condition Assessment
Ultrasonic energy can provide information from below the material surface.
Thickness Measurement
The technique can measure remaining material thickness without destructive sampling.
One-Sided Access in Many Applications
Some ultrasonic examinations can be performed when only one side of a component is accessible.
No Ionizing Radiation
Ultrasonic inspection does not use the X-rays or gamma radiation associated with radiographic examination.
Immediate Data
Technicians can review ultrasonic responses during the inspection.
Repeat Monitoring
Controlled measurement locations can be revisited to monitor thickness or selected equipment conditions over time.
These advantages explain why ultrasonic techniques are commonly integrated into industrial inspection and asset-condition programs.
Limitations of Ultrasonic Testing
Knowing when ultrasonic inspection may be difficult is just as important as understanding its benefits.
Ultrasonic NDT may face limitations involving:
- Complex component geometry
- Rough or inaccessible surfaces
- Difficult acoustic materials
- Unfavorable discontinuity orientation
- Limited scanning access
- Inappropriate probe selection
- Poor coupling
- Incorrect calibration
- Interpretation complexity
Therefore the inspection question should be defined before selecting the technique.
A method should not be chosen simply because ultrasonic equipment is available.
Ultrasonic Testing in Power Generation
Power plants contain piping welded components pressure-related equipment turbines and other assets that may require internal condition assessment or thickness monitoring.
Ultrasonic Testing Applications in power generation can include weld examination corrosion monitoring material thickness measurement and selected component inspections.
The results may then contribute to a broader assessment involving maintenance history operating conditions and other inspection findings.
Facilities requiring assessment beyond an individual UT examination can use Lamassu Energy’s Power Plant Inspection service to support wider plant inspection requirements.
Ultrasonic Inspection for Oil and Gas Equipment
Oil and gas assets may experience corrosion erosion mechanical loading and other operating conditions that require condition assessment.
Relevant Ultrasonic Inspection applications can include pipelines pressure vessels process piping storage equipment and welded components.
Thickness measurements can help monitor wall loss while other ultrasonic techniques can be selected when internal discontinuity evaluation is required.
Inspection planning should account for service history material condition expected degradation mechanisms and applicable requirements.
Ultrasonic Testing in Middle Eastern Industrial Environments
Industrial and energy facilities across the UAE Iraq Jordan Syria Saudi Arabia and other Middle Eastern markets can operate under demanding conditions involving high ambient temperatures continuous production and challenging field environments.
These factors can influence inspection planning equipment access and component condition.
However geography alone should never determine the Ultrasonic Testing Method.
Inspection teams should instead consider actual equipment temperature material surface condition service history accessibility expected damage mechanism and applicable procedures.
This approach keeps the inspection focused on the equipment problem rather than applying generic regional assumptions.
When Should Ultrasonic Testing Be Used?
Ultrasonic examination may be suitable when the inspection objective involves:
- Internal discontinuity evaluation
- Material thickness measurement
- Corrosion monitoring
- Selected weld examination
- In-service component assessment
- Repeated thickness measurements
It may not be the appropriate first choice when the inspection objective is limited to surface-breaking defects that can be more effectively evaluated using another NDT technique.
This distinction is important because the best inspection program does not attempt to solve every problem with one method.
For requirements involving multiple inspection techniques Lamassu Energy provides Non Destructive Testing services for industrial and power generation applications.
How to Select the Right Ultrasonic Testing Method
Choosing the appropriate Ultrasonic Testing Method starts with defining the question the inspection needs to answer.
Define the Inspection Objective
Determine whether the requirement is thickness measurement corrosion monitoring weld evaluation internal defect detection or another condition assessment.
Understand the Material
Material acoustic properties can affect sound transmission and inspection feasibility.
Consider the Expected Discontinuity
Expected defect location orientation and characteristics influence probe and technique selection.
Evaluate Component Geometry
Thickness curvature weld geometry and access can affect the inspection approach.
Review Operating Conditions
Temperature surface condition coatings and field accessibility may influence execution.
Follow Applicable Requirements
The procedure should reflect applicable standards codes specifications and equipment requirements.
This problem-first approach is more reliable than selecting an ultrasonic technology before understanding the inspection requirement.
How UT Testing Supports Maintenance Decisions
The purpose of UT Testing is not simply to produce readings.
The inspection data should answer an equipment question.
For example thickness measurements may help determine whether corrosion requires additional monitoring engineering assessment or maintenance intervention.
A weld indication may require characterization evaluation against applicable criteria or complementary inspection.
The decision process therefore becomes:
Equipment Concern → Inspection Objective → UT Method → Reliable Data → Engineering Evaluation → Appropriate Action
This approach prevents ultrasonic inspection from becoming a routine exercise disconnected from equipment reliability.
Where facilities require specialist field coordination around inspection findings Lamassu Energy’s Technical Field Advisor service can support technical activities associated with critical power generation and industrial equipment.
Why Qualified Ultrasonic Testing Personnel Matter
Modern ultrasonic equipment can provide sophisticated inspection data but technology does not remove the need for competent personnel.
Qualified technicians need to understand:
- Ultrasonic principles
- Calibration
- Probe characteristics
- Material behavior
- Component geometry
- Scanning requirements
- Signal interpretation
- Reporting procedures
This becomes especially important when inspection findings influence maintenance or engineering decisions.
For industrial projects requiring coordinated onsite personnel Lamassu Energy also provides Dedicated Service Crews to support field activities in demanding operating environments.
Common Ultrasonic Testing Mistakes
Starting Without a Clear Inspection Objective
The technique should answer a defined equipment question rather than simply generate inspection data.
Using an Unsuitable Probe
Probe selection must reflect material thickness geometry and expected discontinuity.
Poor Calibration
Incorrect setup can reduce confidence in thickness location or indication information.
Ignoring Geometry
Known geometric features can create signals that inexperienced operators may misinterpret.
Assuming Every Signal Is a Defect
Ultrasonic responses require interpretation. Not every indication represents a rejectable discontinuity.
Relying on One Reading for Corrosion Decisions
Thickness trends and engineering context can provide more useful information than a single measurement.
Using Ultrasonic Testing for Every NDT Problem
Ultrasonic inspection has specific capabilities and limitations. Other NDT methods may be more appropriate for some surface conditions materials or inspection objectives.
Professional Ultrasonic Inspection Support from Lamassu Energy
Effective ultrasonic inspection depends on matching the technique to the equipment problem and combining reliable testing with experienced technical evaluation.
Lamassu Energy supports power generation oil and gas and industrial facilities with technical inspection field support and equipment-focused solutions for demanding operating environments.
Through its Non Destructive Testing services Lamassu Energy supports inspection requirements where equipment condition weld integrity material thickness and asset reliability need professional evaluation.
Combined with power plant inspection technical field advisory and dedicated service crews this capability helps facilities connect inspection findings with wider maintenance and reliability requirements.
Need support evaluating critical industrial equipment? Explore Lamassu Energy’s inspection and field capabilities for your operational requirements.
Frequently Asked Questions About Ultrasonic Testing
What is Ultrasonic Testing?
Ultrasonic Testing is a non destructive inspection technique that uses high frequency sound waves to evaluate materials and components without destructive examination.
What is UT Testing used for?
UT Testing can be used for internal discontinuity detection weld examination material thickness measurement corrosion monitoring and selected industrial equipment inspections.
What is Ultrasonic Thickness Testing?
Ultrasonic Thickness Testing uses sound travel time to determine material thickness and is commonly applied to piping tanks pressure equipment and other assets exposed to material loss.
Can Ultrasonic Testing detect internal cracks?
It can detect certain internal discontinuities including cracks when their characteristics orientation material and inspection setup allow sufficient ultrasonic response.
Can Ultrasonic Testing measure corrosion?
Ultrasonic thickness measurements can identify material thickness loss and support corrosion monitoring when measurements are collected and evaluated appropriately.
What are the main benefits of Ultrasonic Testing?
Benefits include internal condition assessment thickness measurement immediate inspection data one-sided access for many applications and the absence of ionizing radiation.
What are the limitations of Ultrasonic Testing?
Limitations can involve complex geometry surface condition material properties defect orientation accessibility calibration and dependence on technician competence.
Is Ultrasonic Testing suitable for weld inspection?
Yes. Several ultrasonic techniques can be used for weld examination when the material geometry expected discontinuity and inspection procedure are appropriate.
Does Ultrasonic Testing damage equipment?
No. Ultrasonic NDT is intended to evaluate a component without the destructive damage associated with destructive testing.
How do you choose the right Ultrasonic Testing Method?
Selection should consider the inspection objective material expected discontinuity component geometry thickness surface condition accessibility and applicable inspection requirements.